Packaging plant and reliability laboratory, Bao'an, Shenzhen
Automated assembly commissioned in 2021 and expanded in 2024, with reliability testing and failure analysis in the same building as the lines that produce the parts.
Shenzhen Hexin Electronics Co., Ltd. operates an automated power semiconductor packaging plant in Bao'an, Shenzhen, commissioned in 2021 and expanded in 2024, with stated capacity of 50 million units per month. The plant covers die attach, wire bonding, moulding, trim and form, 100% electrical test and marking, with nine reliability test types and X-ray, C-SAM, die shear and wire pull analysis performed on site.
Four areas that decide what a customer receives
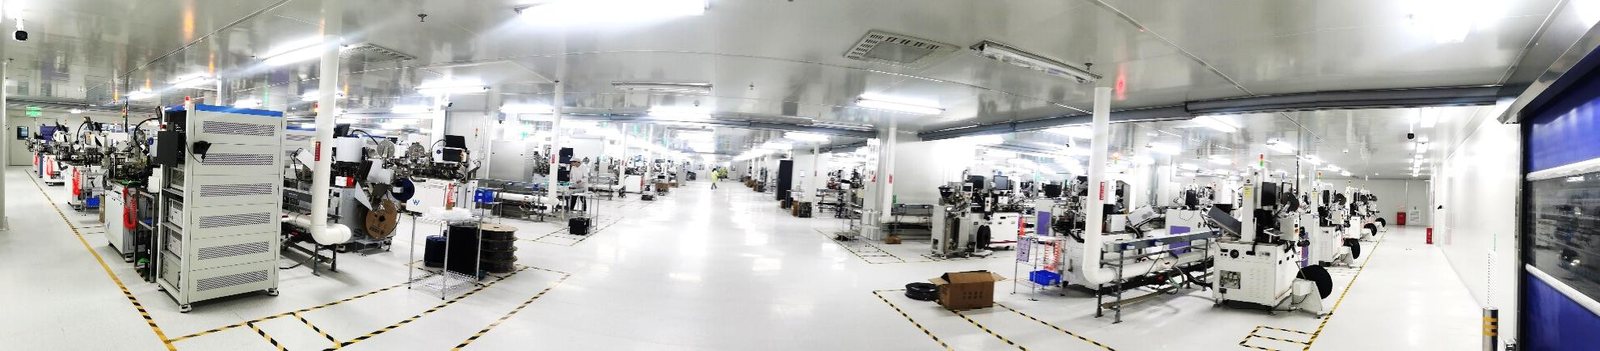
Assembly Hall — Automated lines · since 2021
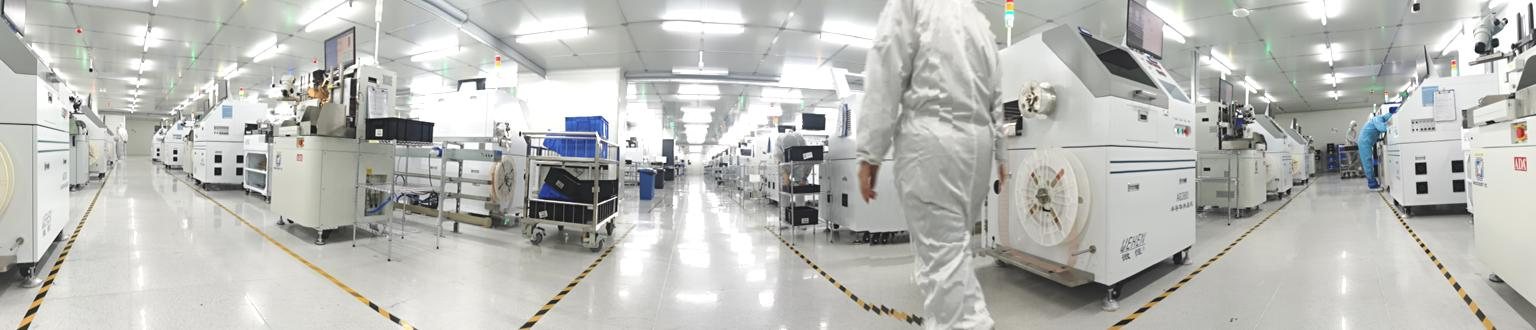
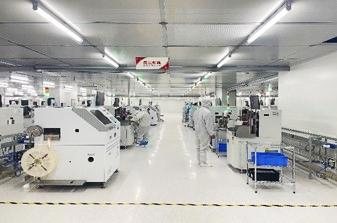
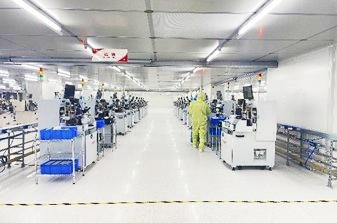
Die attach, wire bonding, moulding and trim/form on automated lines running 50 million units per month.
Assembly is laid out by operation rather than by product, so a lot moves from die attach through bonding, moulding and singulation in one direction with no backtracking. Each station reads the lot code from the carrier and the MES blocks a mismatch against the work order, which is the control that stops mixed lots. Equipment was expanded in 2024 to raise stated capacity to 50 million units per month across TO-220, TO-252, TO-263, TO-247, PDFN and TOLL outlines.
Electrical Test — 100% final test
Every unit tested for breakdown, on-resistance, threshold and leakage before marking.
Final electrical test is where a packaging operation either earns its reputation or loses it, because the parameters that matter to a power supply designer — RDS(on), VGS(th), BVDSS, IDSS — are all measurable at this point. Test programmes are written per part number with limits taken from the datasheet, and a failing unit is binned rather than re-marked. Handlers are dedicated per package family to avoid conversion error.
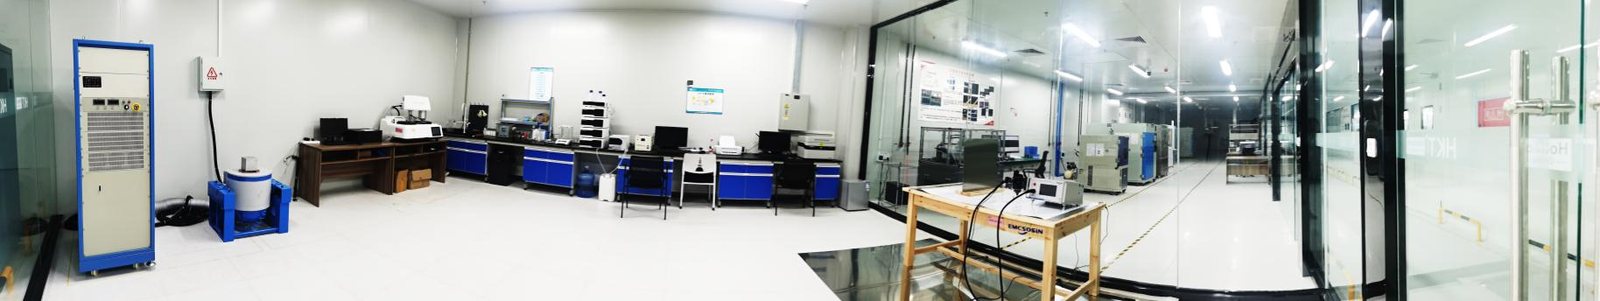
Reliability Laboratory — 9 test types
HTRB, H3TRB, HT/HU, HTSL, thermal cycling, thermal shock, solderability, RSH and HPC.
The reliability lab runs qualification and lot monitoring in-house instead of sending samples to a third party, which shortens the loop between a failure and the analysis of that failure. Bias ovens monitor each device under HTRB, humidity chambers run H3TRB with bias, and thermal cycling and shock cover the mechanical stress side. Reports state sample size, conditions and read points, because a reliability claim without those three numbers is marketing.
Failure Analysis — X-ray · C-SAM · shear/pull
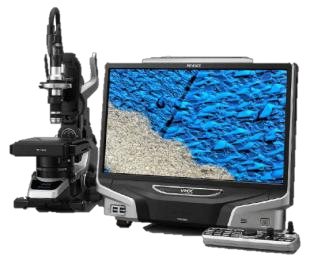
X-ray (YXLON), acoustic scanning (Sonoscan PVA), die shear, wire pull and optical microscopy.
Failure analysis is what makes the reliability data usable. X-ray shows die attach voiding and wire sweep without opening the package; C-SAM (Sonoscan PVA) images delamination between the mould compound and the die surface, which is the usual root cause of a humidity failure; die shear and wire pull quantify bond strength against JESD22 limits. Optical microscopy covers the rest — cracks, corrosion, marking defects.
Production and laboratory floor, photographed on site
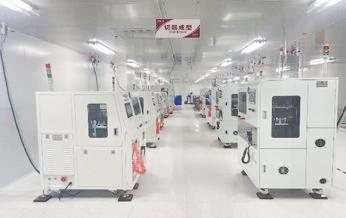
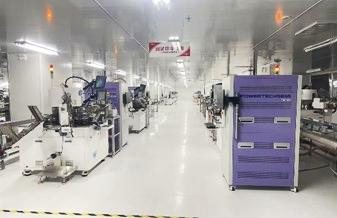
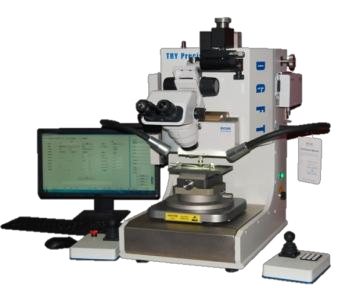
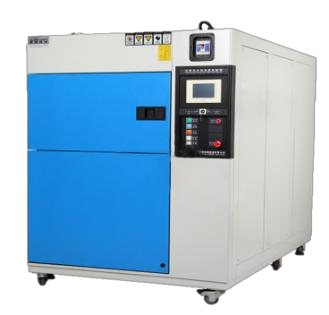
Photographs from the production hall and the laboratory verification area. Equipment names are stated only where the brochure identifies them; the rest are shown as they stand rather than labelled with guessed model names.
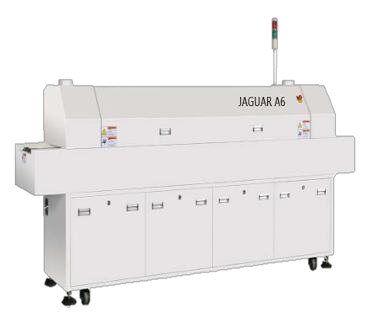
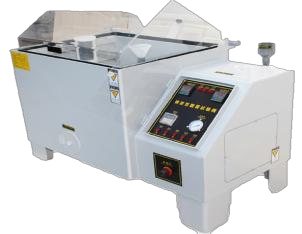
Equipment list
Grouped by operation. Where the knowledge base does not record a count, the list says what the equipment does rather than inventing a number.
| Equipment | Scope | Purpose |
|---|---|---|
| Automatic die attach stations | Automated lines | Solder and high-temperature attach, X-ray void sampling |
| Copper wire bonders | Automated lines | Wire pull and die shear monitoring per shift |
| Transfer moulding presses | Automated lines | UL 94V-0 compound, post-mould cure ovens |
| Trim / form / singulation | Per outline | TO-220 series, TO-247, TO-252, TO-263, PDFN, TOLL4 |
| Automatic test handlers | Per package family | 100% final electrical test before marking |
| Laser marking | Automated | Date code and lot code on every unit |
| X-ray inspection (YXLON) | 1 system class | Die attach voiding and wire sweep |
| C-SAM (Sonoscan PVA) | 1 system class | Delamination imaging between compound and die |
| Thermal cycling chamber (TCT) | In-house | Air-to-air cycling, cycle count recorded per lot |
| HTRB / H3TRB chambers | In-house | Bias stress with per-device monitoring |
| Die shear and wire pull testers | In-house | JESD22 bond strength limits |
| Optical microscope | In-house | Crack, corrosion and marking inspection |
Address: Building 2, Bao'an Runhui Technology Park, Hongqiaotou Community, Yanluo Street, Bao'an District, Shenzhen, Guangdong, China. Visits and audits are arranged by appointment; remote video walkthroughs of the assembly and test areas are available for a first screening.
Want to audit the plant before ordering?
We arrange visits and remote walkthroughs of the assembly hall, electrical test and reliability laboratory. Tell us which operations your audit procedure requires and we will confirm what can be shown, and what belongs to a foundry partner.